


 English
 русский
 Español
 عربى

Zinc & Aluminum Die Cast Parts
-- Steady & Reliable Manufacturer --
Yuyao Hongli Optoelectronics Co., Ltd. is a premier manufacturer of Zinc & Aluminum Die Cast Parts, specializing in high-density, thin-wall, and high-strength metal castings for automotive assemblies, lighting housings, power tools, and electronic enclosures. Operating from our 5,000-square-meter facility in Yuyao, Zhejiang, we run automated cold-chamber aluminum and hot-chamber zinc die casting machines ranging from 88T to 800T. We cast premium alloys including ADC12, A380, A360, Zamak 3, and Zamak 5 into intricate components featuring smooth surface finishes, high dimensional accuracy, and zero internal porosity. Partner with Yuyao Hongli for integrated mold design, precision CNC post-machining, powder coating, and direct-factory OEM supply.
-
 View More
-
 View More
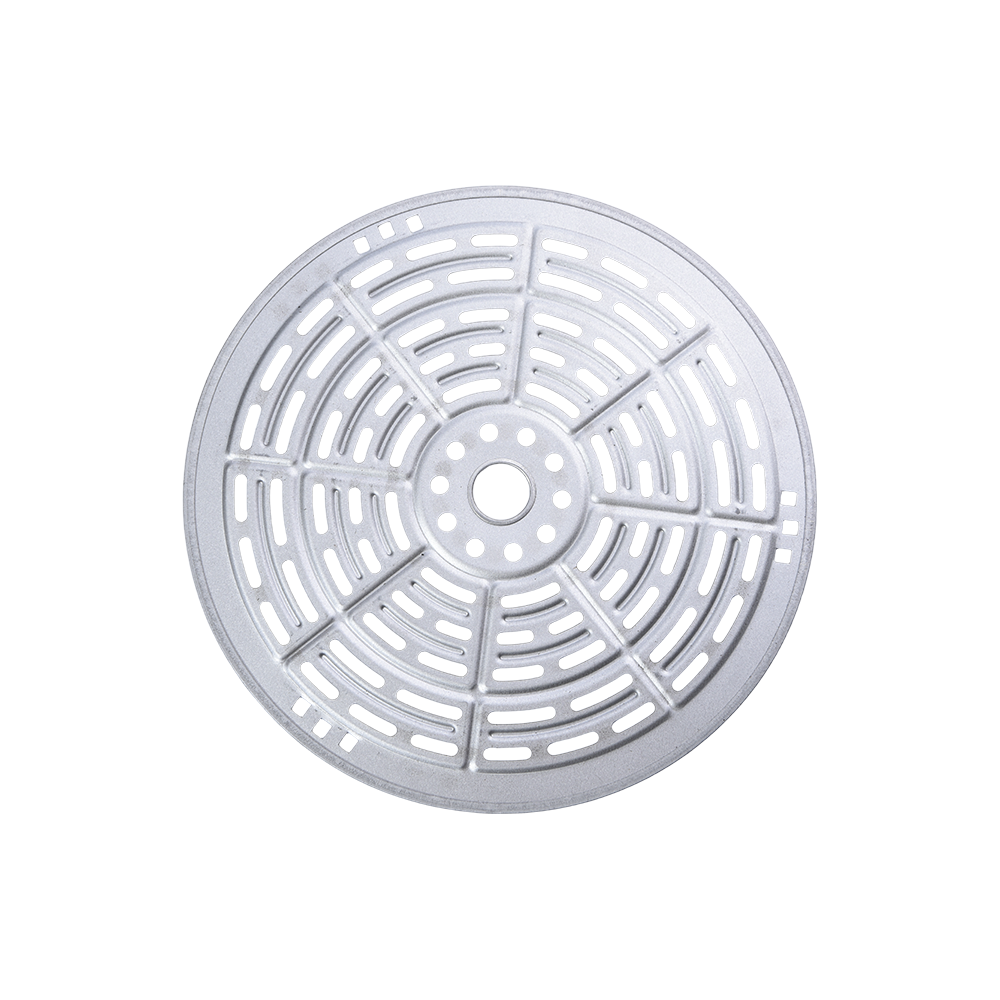
Stamped circular parts with holes
-
 View More
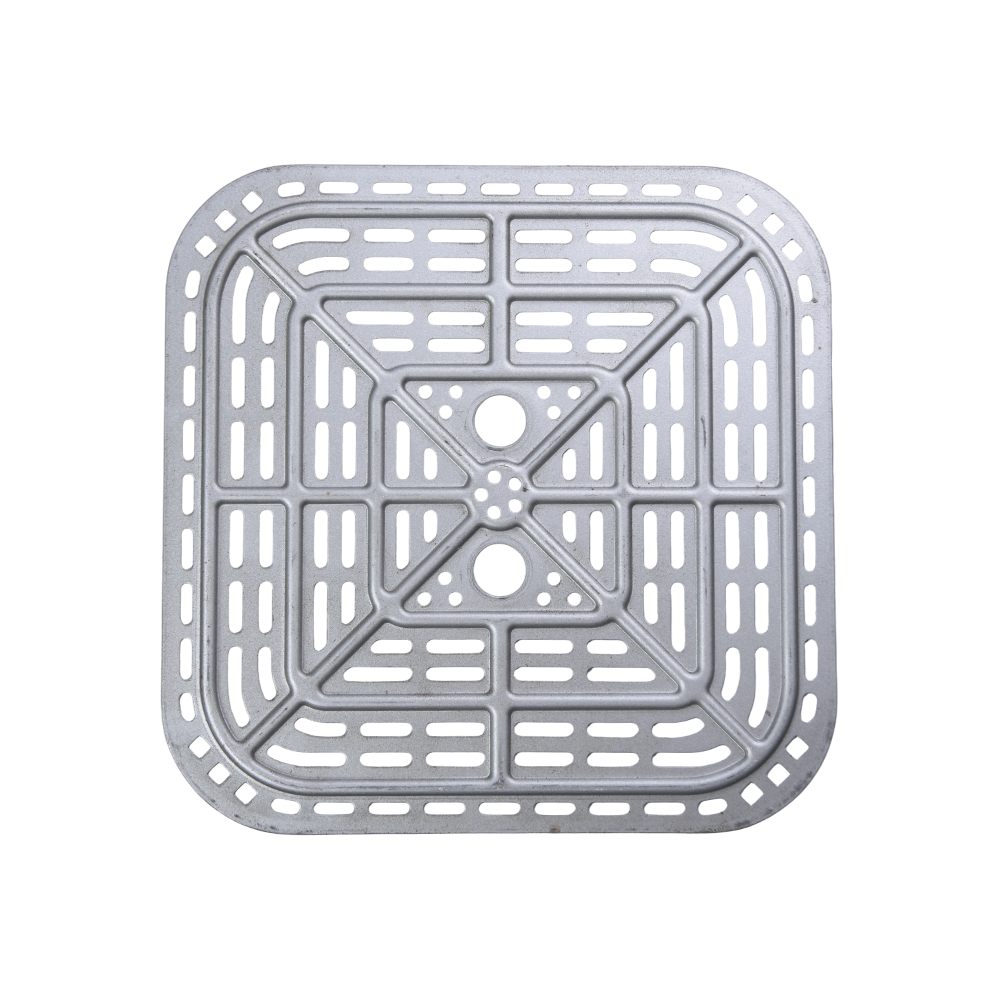
Stamped square parts with holes
-
 View More
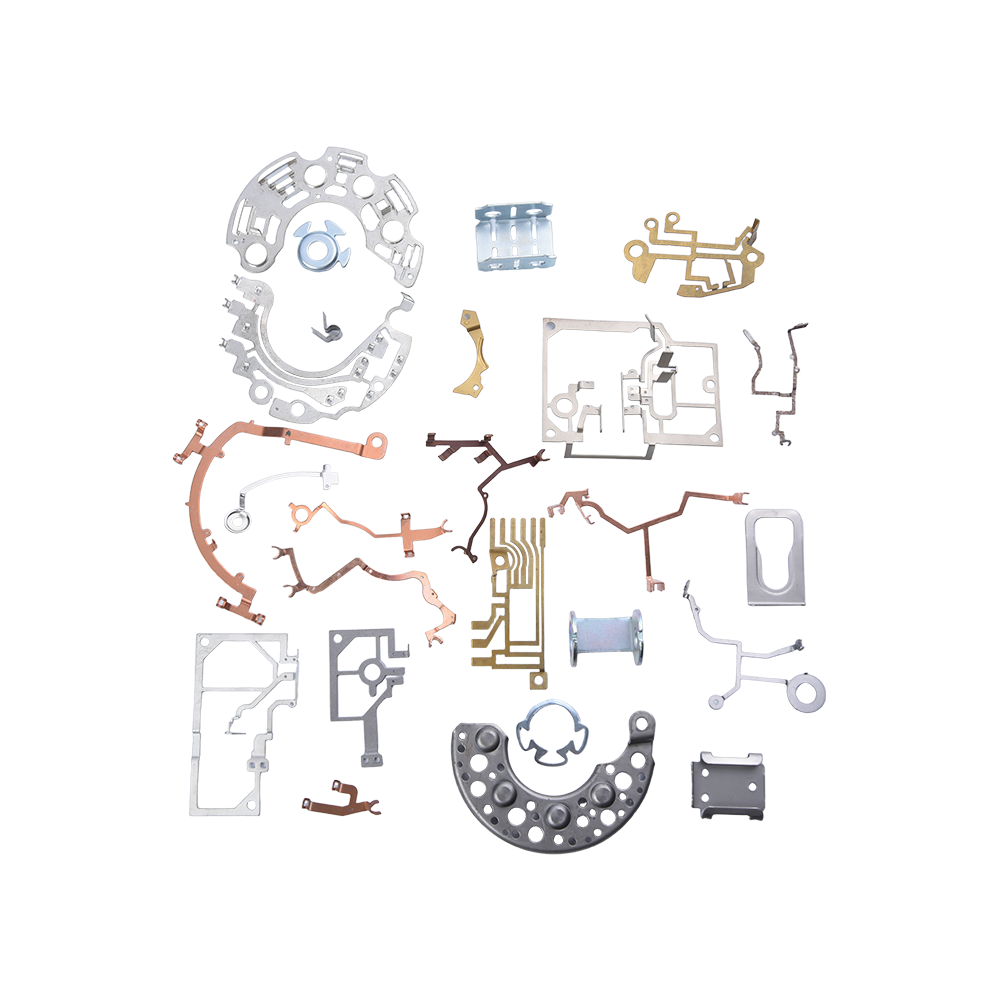
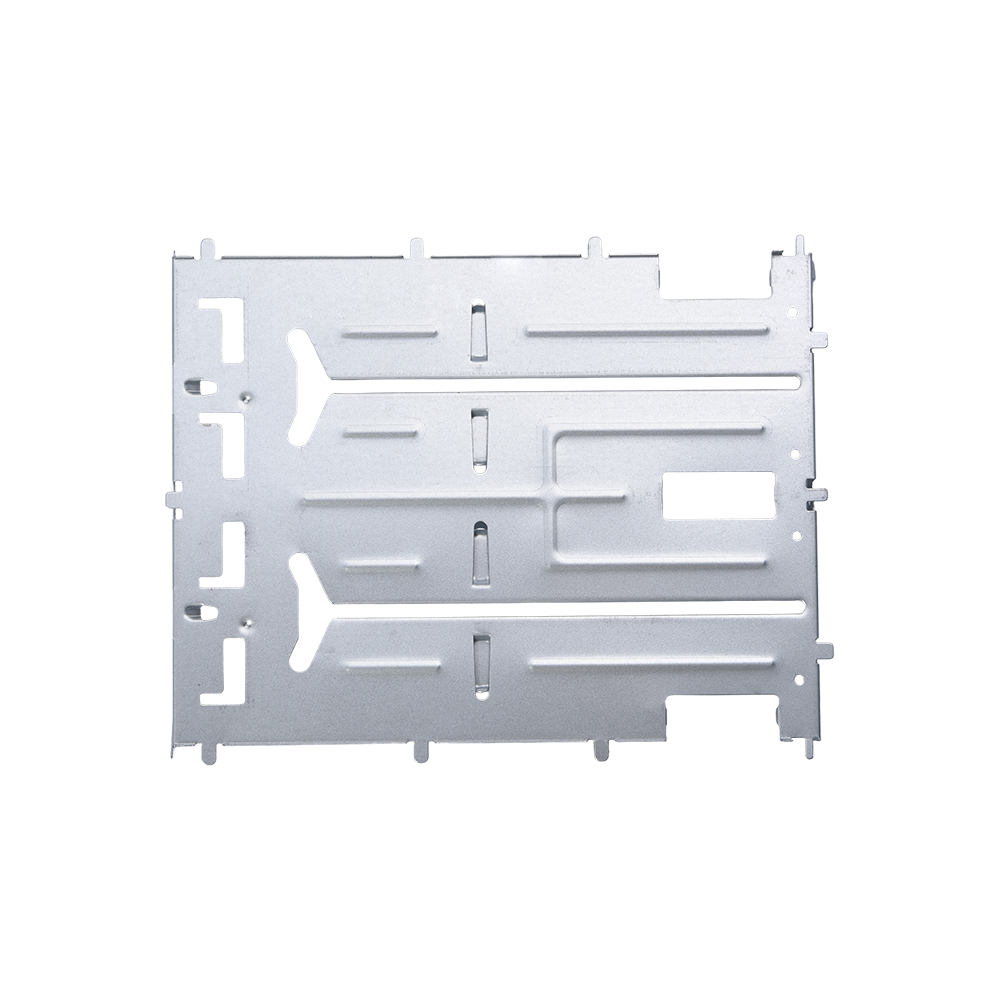
Stamped ultra-thin parts
-
 View More
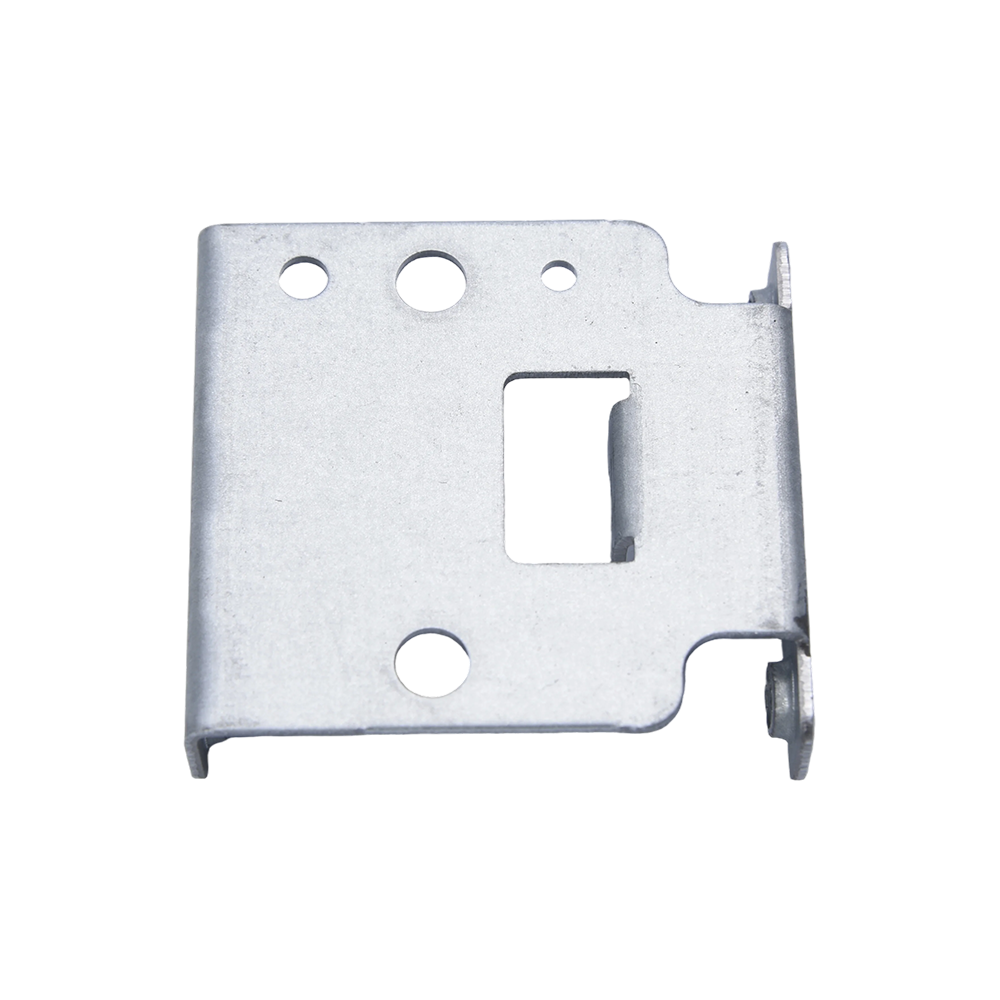
Stamped small square parts
-
 View More
Stamped miniature parts
-
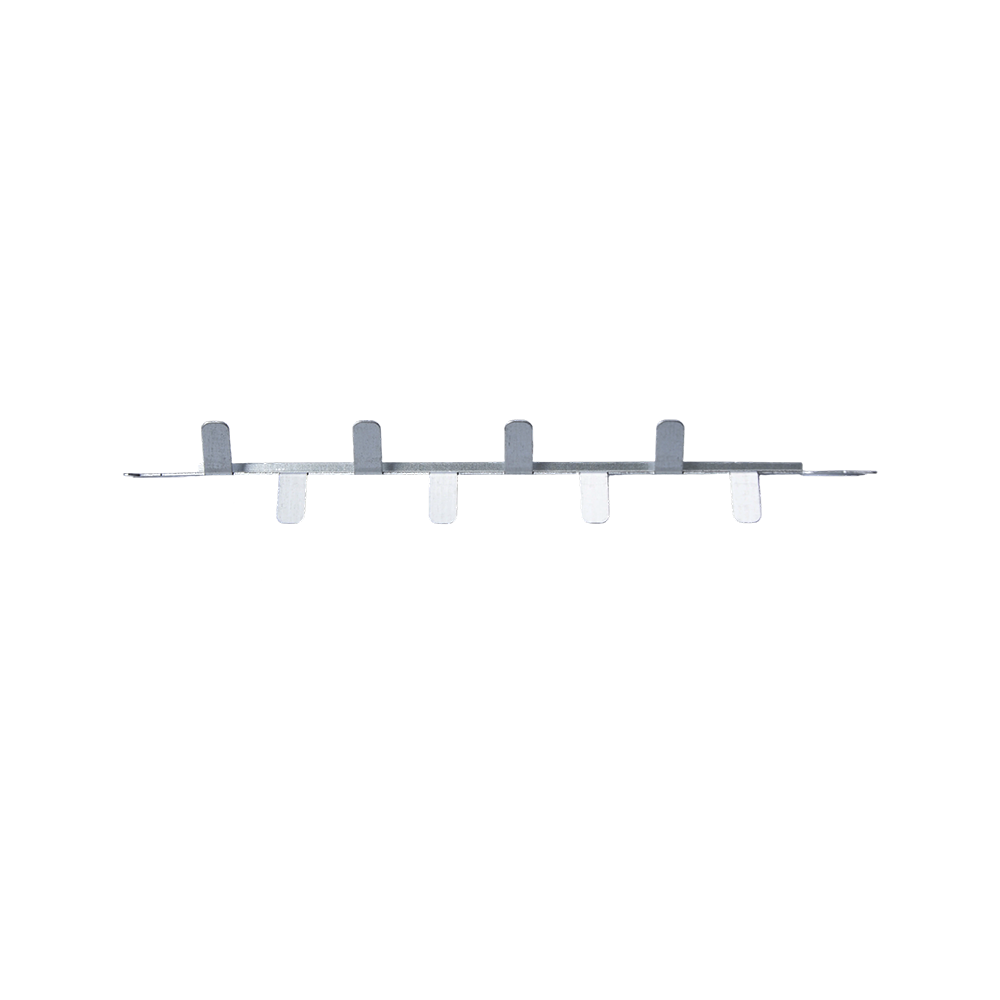 View More
Stamped bendable strip-shaped parts
-
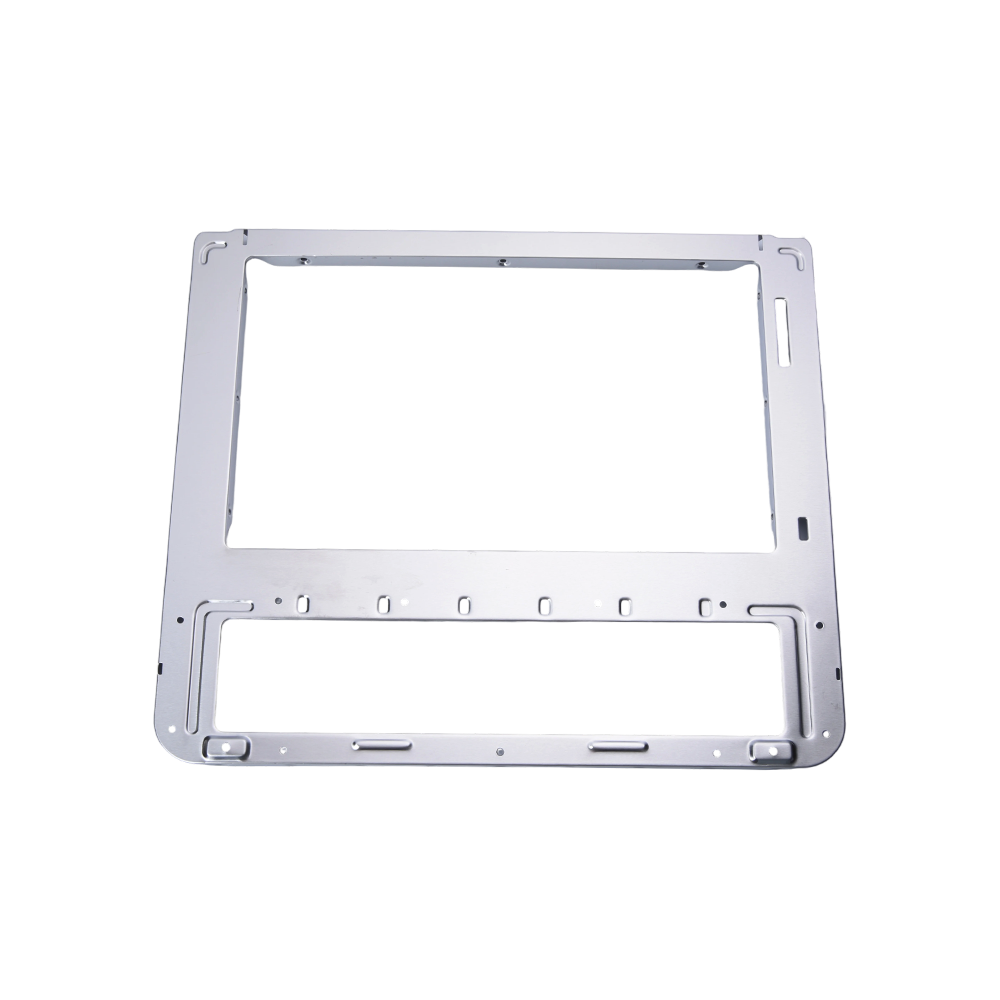 View More
Square-shaped precision machined stamped parts
-
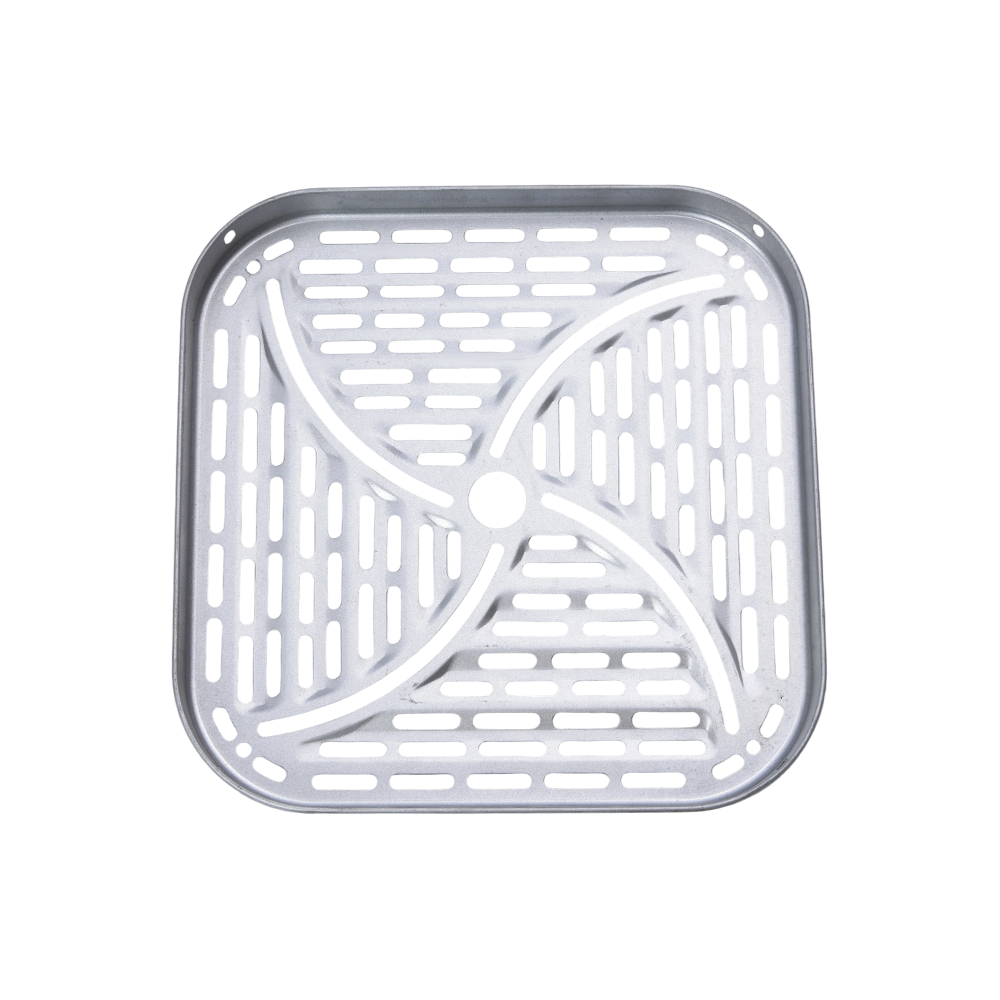 View More
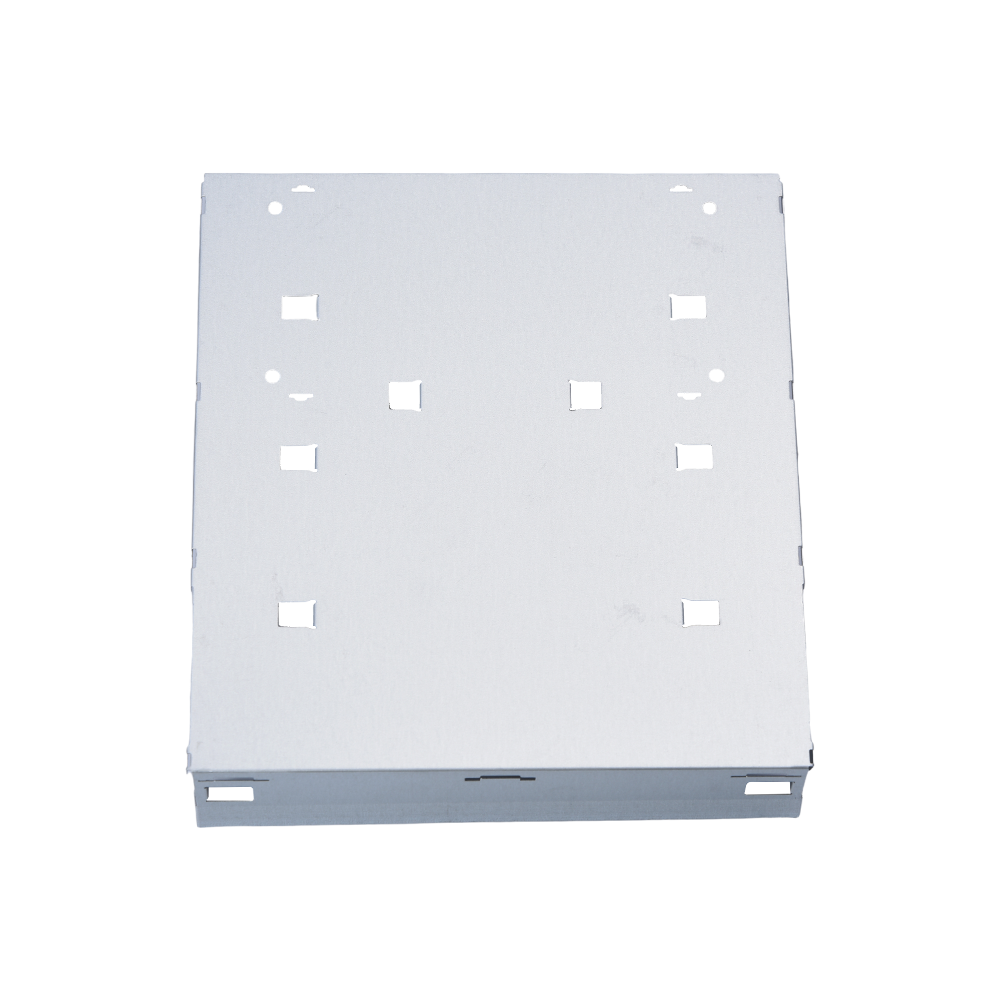
Stamped chassis parts
-
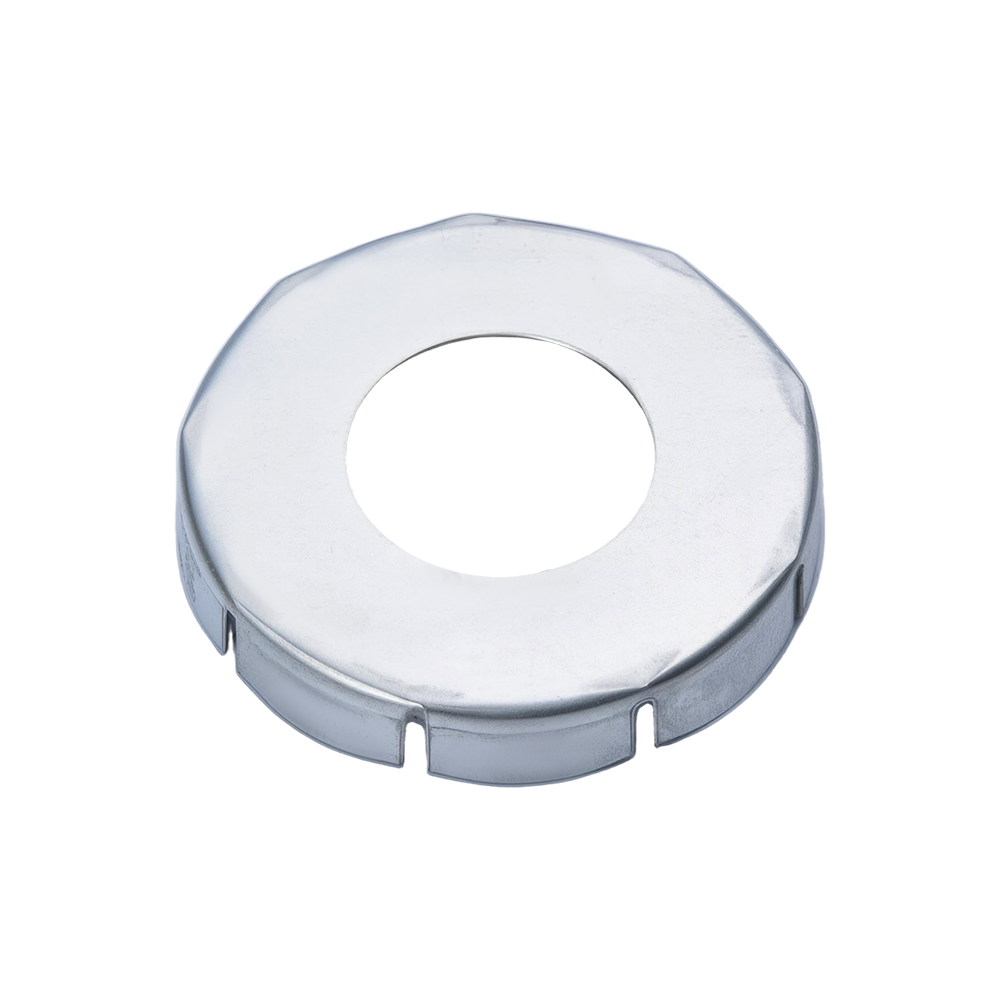 View More
Circular stamped parts with a central hole
MANUFACTURING CAPABILITIES
Equipment and process capabilities
From mold design to batch stamping, we cover production needs of different tonnages and precision levels.
- 01
High-Pressure Cold Chamber Aluminum Die Casting
Utilizing high-tonnage cold chamber die casting machines up to 800T, we inject molten aluminum alloy at high speed to produce complex, thin-walled structural housings with high strength-to-weight ratios.
- 02
Hot Chamber Zinc Alloy Precision Die Casting
Our hot chamber zinc casting machines produce high-precision, intricate hardware parts with tight tolerances, excellent impact strength, and exceptional surface fluidity for ultra-thin walls down to 0.8mm.
- 03
Secondary CNC Milling & Turning Post-Machining
Equipped with 4-axis CNC machining centers, we perform precision trimming, thread tapping, face milling, and bore reaming to achieve critical assembly tolerances down to ±0.01mm.
- 04
Automated Shot Blasting & Electrostatic Powder Coating
We operate automated shot blasting machinery to remove flash and smooth cast surfaces, followed by weather-resistant powder coating or anodizing for superior corrosion protection.
SPEC · Overview of Key Equipment Parameters
| Equipment Type | Tonnage / Specification | Machinable Material | Typical Processing Thickness |
|---|---|---|---|
| Cold Chamber Die Casting Machine | 160T - 800T High-Pressure Casting | Aluminum Alloys (ADC12, A380, A360, AlSi10Mg) | 1.2mm - 8.0mm Wall Thickness |
| Hot Chamber Die Casting Machine | 88T - 250T Automatic Casting | Zinc Alloys (Zamak 3, Zamak 5, ZA-8) | 0.8mm - 5.0mm Wall Thickness |
| 4-Axis CNC Machining Center | 12,000 RPM High-Speed Spindle | Cast Aluminum & Zinc Components | Post-Machining Precision ±0.01mm |
| X-Ray Porosity Inspection Unit | 160kV Real-Time Industrial X-Ray | Structural Die Cast Parts | Internal Defect Detection |
QUALITY CONTROL
Full-process quality control system
From incoming material inspection to full outgoing inspection, key processes are equipped with inspection points to ensure batch consistency.
X-Ray Non-Destructive Porosity Inspection
Detecting internal gas pores and shrinkage defects inside critical load-bearing castings.
- 160kV real-time X-ray inspection ensuring structural density compliance.
- Density checks and sectioning analysis for pressure-tight liquid/gas housings.
- Helium leak testing for sealed automotive and pump enclosures.
3D CMM & Optical Dimension Audit
Verifying strict geometric tolerances across complex casting contours.
- Coordinate Measuring Machine (CMM) inspection for hole locations and flatness.
- 3D laser scanning against customer 3D CAD models to check shrinkage compensation.
- Thread pitch diameter checking after secondary tapping operations.
Salt Spray & Surface Finish Quality Testing
Ensuring exterior painted and electroplated die castings withstand outdoor exposure.
- Neutral Salt Spray (NSS) testing per ASTM B117 (up to 720 hours for powder coated aluminum).
- Cross-hatch adhesion testing (ISO 2409) for painted and e-coated castings.
- Surface roughness measurement (Ra 1.6 to 3.2 µm standard cast finish).
SURFACE FINISHING
Surface treatment process
Depending on the usage environment and appearance requirements of the parts, we offer anti-corrosion, wear-resistant, or decorative surface treatment solutions.
| Finishing Process | Applicable Material | Primary Function | Typical Application |
|---|---|---|---|
| Electrostatic Powder Coating | Aluminum Alloys, Zinc Alloys | Provides durable, UV-resistant, colorful protective shell against corrosion | Outdoor LED light housings, automotive motor covers, power tool bodies |
| Chromate Conversion Coating (Chemical Film) | Cast Aluminum (ADC12, A380) | Improves paint adhesion and provides corrosion resistance without changing dimensions | Electronic heat sinks, internal automotive module frames, telecom enclosures |
| Copper-Nickel-Chrome Electroplating | Zinc Alloys (Zamak 3, Zamak 5) | Delivers brilliant mirror-like chrome finish with high scratch resistance | Automotive door handles, bathroom hardware fixtures, decorative emblems |
| Anodizing / Hard Anodizing | Cast Aluminum Alloys | Creates hard anti-wear oxide layer with excellent dielectric insulation properties | High-performance engine brackets, hydraulic valve bodies, heatsinks |
Note: The above is a standard process list. Specific film thickness, color, and salt spray resistance rating can be customized according to customer drawings.
APPLICATIONS
Main application areas
Our products are widely used in industries that require high structural strength and precision consistency.
Automotive Powertrain & Structural Housings
Lightweight, high-strength aluminum and zinc die castings engineered for vehicle platforms.
- Automotive electronic control unit (ECU) heat-sink enclosures
- Transmission shift lever brackets and wiper motor housings
- Electric vehicle (EV) battery module cooling end plates
Industrial Lighting & Power Tool Housings
Rugged die-cast metal enclosures built for heavy outdoor and industrial environments.
- Outdoor LED street light heat-sink fixture housings
- High-bay industrial light driver enclosures
- Pneumatic tool handles and gear case housings
Electronics & Precision Hardware Components
Tight-tolerance zinc die-cast lock components and telecom electronics shielding.
- Smart door lock bodies, escutcheons, and latch hardware
- 5G telecom RF filter housings and shielding covers
- Precision optical instrument mounting frames
PRODUCTION / FACTORY ADVANTAGES
Factory production advantages
With its own factory and equipment, the company ensures stable delivery times and controllable costs.
20+ Years of Die Casting & Mold Engineering
Yuyao Hongli brings over two decades of casting experience, mold flow simulation, and alloy processing in Yuyao, Zhejiang.
Complete In-House Tooling & CNC Machining
We handle mold design, die casting, precision CNC post-machining, and surface finishing within our integrated plant.
X-Ray & CMM Backed Quality Assurance
Equipped with industrial X-ray inspection and 3D CMM machines to guarantee defect-free, pressure-tight castings.
CUSTOM MANUFACTURING PROCESS
Customized production process
From receiving drawings to batch delivery, standardized processes ensure traceability at every stage.
1. Part Design & Mold Flow Simulation
We review customer 2D/3D CAD files and run computer mold flow analysis to optimize gating, runner, and overflow design.
2. Die Casting Mold Tooling Fabrication
Our toolmakers machine high-durability H13 tool steel molds with conformal cooling channels to ensure long mold life.
3. Trial Casting, X-Ray & FAI Inspection
First sample castings undergo X-ray porosity testing, CMM dimensional checks, and surface finish checks for customer approval.
4. Mass High-Pressure Casting & CNC Machining
Automated casting cells produce parts at high cycle rates, followed by robot trimming and CNC precision machining.
5. Powder Coating, Quality Audit & Shipping
Parts undergo shot blasting, powder coating or plating, pass 100% final inspection, and are packed in custom protective boxes.
FAQ
Frequently Asked Questions
Here are some questions that clients often ask before cooperating with us.
What is the main difference between zinc and aluminum die casting?
Zinc alloys have a lower melting point, allowing thinner walls (0.8mm) and longer mold life, while aluminum alloys offer lighter weight and higher temperature tolerance.
How do you control internal porosity in aluminum die cast parts?
We use mold flow simulation, vacuum-assisted die casting, controlled shot speeds, and verify internal density using real-time industrial X-ray equipment.
What precision can be achieved after secondary CNC machining on castings?
Our 4-axis CNC machining centers achieve post-machining tolerances down to ±0.01mm on critical bores, bearing seats, and sealing faces.
What aluminum and zinc alloys do you commonly use?
Common aluminum alloys include ADC12, A380, A360, and AlSi10Mg. Common zinc alloys include Zamak 3, Zamak 5, and ZA-8.
About Us
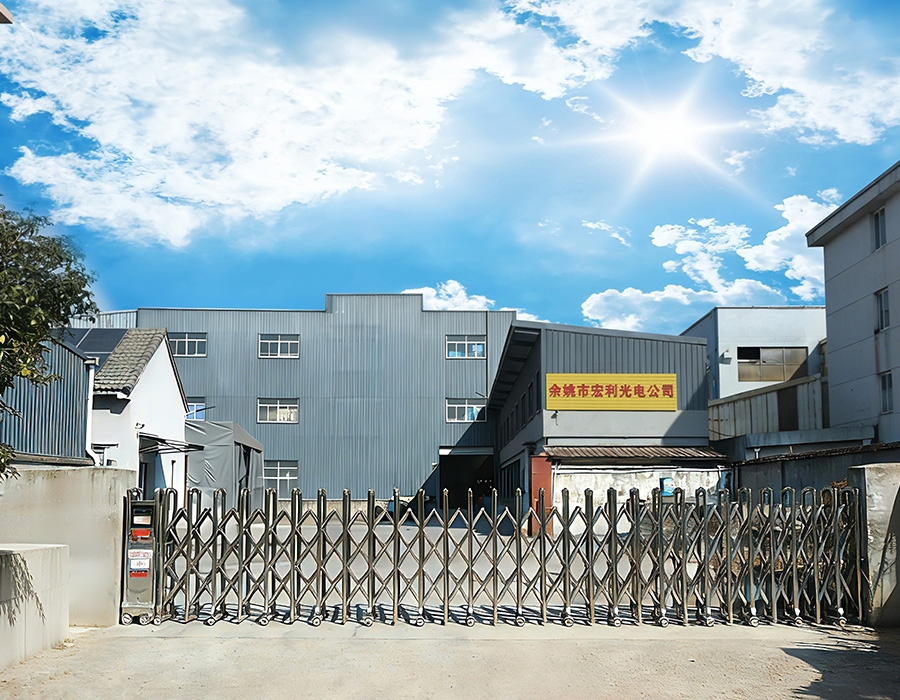
Yuyao Hongli Optoelectronics Co., Ltd.
Yuyao Hongli Optoelectronics Co., Ltd. is a comprehensive enterprise with over 20 years of experience in the manufacturing industry. Located in the Yangming Science and Technology Industrial Park of Yuyao, Zhejiang Province, it enjoys convenient transportation and a solid industrial foundation. As a famous China Zinc & Aluminum Die Cast Parts Suppliers and Zinc & Aluminum Die Cast Parts Factory, founded in 2000, formerly known as Yuyao Hongli Optoelectronics Educational Instruments Co., Ltd., the company is wholly owned by a natural person, with Xie Gang as the legal representative. Its registered capital of 500,000 yuan has been fully paid up, and it has maintained its continued development through stable operations.
Relying on a 5,000-square-meter modern factory and multiple stamping workshops, the company has built a diversified product system. Its core businesses cover the manufacturing, processing and wholesale and retail of educational instruments, optical instruments, household electric heaters, small household appliances, auto parts, hardware and plastic products, etc. At the same time, it operates and acts as an agent for the import and export trade of goods and technologies, and its products are sold at home and abroad.
The company brings together industry management elites and senior engineers to form a mature R&D and management team. Adhering to the business philosophy of "integrity and pragmatism," it is committed to providing customers with high-quality products and comprehensive after-sales service. Leveraging its diversified portfolio, certification guarantees, and import/export advantages, the company actively expands cooperation both domestically and internationally, and is willing to establish long-term and stable trade partnerships with partners from all sectors, continuously striving forward in the wave of intelligent and high-end development in the manufacturing industry.
GET IN TOUCH
